
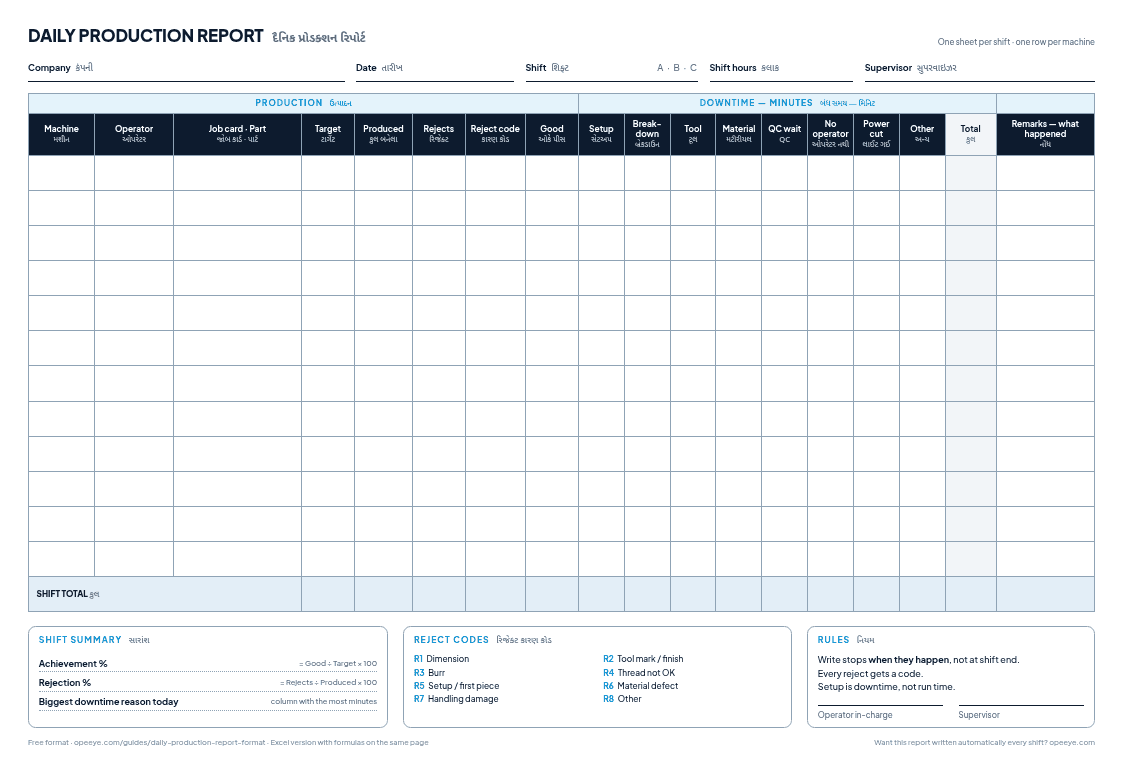
A daily production report (DPR) records, for each machine and shift: operator, job and part, target, pieces produced, rejects with a reason, good pieces, and downtime minutes split by reason (setup, breakdown, tooling, material, QC wait, no operator, power cut). From those it works out achievement % (good ÷ target) and, with the cycle time, OEE. Then it totals the day and shows where the time went.
What does a daily production report look like?
One day at a small CNC shop in Rajkot: two shifts on a turning centre and one on a VMC, eight-hour shifts with 450 minutes of planned working time. This is the Example sheet inside the Excel template, so you can check every number yourself.
| Machine · Shift | Part | Target | Produced | Rejects | Good | Achieved | Downtime (min) | OEE |
|---|---|---|---|---|---|---|---|---|
| TC-01 · A Suresh | Shaft pin Ø25 JC-0231 · 45 s cycle | 540 | 480 | 9 Dimension | 471 | 87.2% | 62 setup 35 · tooling 15 · material 12 | 78.5% |
| TC-01 · B Ramesh | Shaft pin Ø25 JC-0231 · 45 s cycle | 540 | 540 | 4 Tool mark / finish | 536 | 99.3% | 29 QC wait 11 · power cut 18 | 89.3% |
| VMC-03 · A Priya | Flange Ø80 JC-0228 · 150 s cycle | 160 | 112 | 3 Dimension | 109 | 68.1% | 148 setup 48 · tooling 40 · no operator 60 | 60.6% |
| Day total | 1240 | 1132 | 16 | 1116 | 90.0% | 239 | 76.1% |
What should the owner read from this report?
Not every number. Give the sheet to an owner with a red pen and these are the three things circled.
Same machine, same part, 65 fewer good pieces on shift A.
TC-01 stood for 62 minutes on shift A and 29 on shift B: 35 for the changeover, 15 for a broken insert, 12 waiting for material. Those extra 33 minutes cost about 44 pieces, most of the gap. Look at the stops before you look at the operator.
VMC-03 stood for 148 minutes; 100 of them waiting for a person or a tool.
An hour with no operator (moved to TC-02) and 40 minutes for a tool are a scheduling problem and a tool-crib problem. At a 150-second cycle that is about 40 more flanges: 68% of target would have been about 92%.
Setup is the biggest column: 83 of the day's 239 stopped minutes.
Then no operator (60) and tooling (55). Those three are the agenda for tomorrow’s morning meeting. The 12 rejects for dimension are a question for the setter.
Where the time went · 239 min stopped
- Setup / changeover83 min
- No operator60 min
- Tool broke / not available55 min
- Power cut18 min
- Waiting for material12 min
- Waiting for inspection11 min
Rejects by reason · 16 pcs
- Dimension12 pcs
- Tool mark / finish4 pcs
What goes in each column?
Navy columns are the ones you fill in. Grey columns calculate themselves; don’t type over them.
- Machine · Shift · Operator
- TC-01, A, Suresh. One row per machine per shift, so machines, shifts and people compare fairly.
- Job card · Part
- JC-0231, Shaft pin Ø25. Ties every loss back to the order it was made for.
- Cycle time (sec)
- The ideal seconds per piece for that job, from the program or the quote. Only needed for OEE; leave it blank until you track OEE.
- Target
- Pieces planned for the shift.
- Produced
- Every piece made, good and rejected.
- Rejects · Reason
- How many, and the main reason picked from the list. A count without a reason can't be fixed.
- Downtime, by reason
- Minutes stopped, in the column for the reason: setup, breakdown, tooling, material, QC wait, no operator, power cut or other.
- Remarks
- What happened, with the time: “Insert broke 11:40”.
- Good · Achievement · Rejection
- Produced − rejects, good ÷ target, rejects ÷ produced.
- Run time · A · P · Q · OEE
- From the cycle time and the downtime. Worked through below.
How to calculate achievement %, rejection % and OEE
The grey columns in the template are these formulas. Here they are with row 1’s numbers, so you can check the arithmetic before you trust the spreadsheet.
Worked on row 1: TC-01, shift A, Shaft pin Ø25, 45 s cycle, target 540, 480 produced, 9 rejected.
Good pieces
Produced − Rejects
471
480 − 9 =H7-I7
Achievement %
Good ÷ Target
87.2%
471 ÷ 540 =K7/G7
Rejection %
Rejects ÷ Produced
1.9%
9 ÷ 480 =I7/H7
OEE, once you write the cycle time and downtime
- Planned timeShift − planned breaks480 − 30
=C3-G3450 min - DowntimeSum of the downtime columns35 setup + 15 tooling + 12 material
=SUM(N7:U7)62 min - Run timePlanned time − Downtime450 − 62
=$K$3-V7388 min - AvailabilityRun time ÷ Planned time388 ÷ 450
=W7/$K$386.2% - PerformanceProduced × Cycle time ÷ Run time480 × 45 s = 360 min, ÷ 388
=H7*F7/60/W792.8% - QualityGood ÷ Produced471 ÷ 480
=K7/H798.1% - OEE = Availability × Performance × Quality86.2% × 92.8% × 98.1% = 78.5%
Why achievement is 87.2% but OEE only 78.5%
The target of 540 was set at 90% of the 600 pieces a 45-second cycle allows in 450 minutes. Achievement measures against your plan; OEE measures against the machine. Track achievement every day, and use OEE to compare machines and find hidden capacity. More in how to calculate OEE.
Daily production report software vs Excel vs paper: which should you use?
| Paper sheet | Excel template | OpeEye (tablet at each machine) | |
|---|---|---|---|
| Cost | Free | Free | ₹399 per machine a month |
| Who fills it | Operator, by hand | Supervisor types it in | Operator taps as it happens |
| Short stops | Usually missed | Usually missed | Recorded |
| Report ready | When someone adds it up | Same day, if typed | Live, and at every shift end |
| Best for | Starting out | Up to about 10 machines | CNC and VMC shops that want it without chasing |
Not a CNC shop, or your register looks nothing like this one? We can build it as an app for you.
Can this report be an app made for your factory?
Yes. Most factories don’t need a big ERP. They need the register they already keep, on a phone, adding itself up, with the day’s report on WhatsApp when the shift ends. Tell us what your supervisors write down today and we’ll build that, in Gujarati if your operators prefer it.
Registers we turn into apps
- 1Daily production reportinstead of the DPR register
- 2Job cards and work ordersinstead of the job-card file
- 3Job-work challan, inward and outwardinstead of the challan book
- 4Inspection reports with photosinstead of the QC file
- 5Attendance and piece-rate wagesinstead of the muster and a calculator
- 6Stock, dispatch and pending ordersinstead of the stores register
How it works
- 1Send a photo of your register or Excel sheet on WhatsApp.
- 2We call you, understand how your floor runs, and show you a first version with your own columns.
- 3You get a fixed price before any work starts. The data stays yours.
Talk to us in English, Hindi or Gujarati. Built and supported from Rajkot, for factories in India and abroad.
Running CNC or VMC machines? You don’t need a custom build. OpeEye already writes this report from taps at each machine, at ₹399 per machine a month. Book a demo
Six rules that keep the report honest
- 1.
Write it when it happens
The operator notes a stop or a reject at the machine, not the supervisor from memory at 9 pm.
- 2.
Every reject gets a reason
Pick from a short list. Free text only goes in remarks.
- 3.
Every stopped minute gets a column
If it fits none, write it under Other with a remark.
- 4.
Setup is downtime
Book changeovers in the Setup column, never as run time.
- 5.
Same basis every shift
Same cycle times, same reason list, same clock. Otherwise the comparisons are noise.
- 6.
Read it every morning
Five minutes with the supervisor: the biggest downtime column, the lowest achievement, any reject reason that repeats.
Downtime in round numbers like 30, 60, 90 and rejects with no reason? That report was written from memory.
Download the template
The Excel file has a blank Daily Report sheet for 20 machine-shifts, the filled Example from this page, a How to use sheet and an editable reject-reason list. Make a copy of the Daily Report sheet for each day. The printable sheet is one page per shift, with labels in English and ગુજરાતી and the reject reasons as codes R1 to R8.
OpeEye · live
This report, filled by the machine.
- VMC-02Valve body21/32Running
- TC-01Shaft pin Ø2547/72Running
- VMC-03Flange Ø809/21Tool change · 4 min
- TC-04Bush Ø400/40Setup · first piece
Every piece counted, every stop asked “why?” on a tablet, and the hourly and daily report on your phone — for 5 machines or 500.
Explore OpeEyeBook a 20-minute demo₹399 ($5 outside India) per machine a month · free 15-day trial
Want this as an app for your factory?
Send us a photo of your register. We build it around your columns, at a fixed price agreed before work starts.
+91 95867 57458What we build →Questions shop owners ask
What is a daily production report (DPR)?
+
A daily production report (DPR on most shop floors) is a one-page record of what each machine was planned to make, what it actually made, how many pieces were rejected and why, and where time was lost. It is written per machine per shift and totalled for the day, so the owner can see in two minutes which machine, job or reason cost output.
What should a daily production report for a CNC or VMC shop contain?
+
Per machine and per shift: operator, job card and part, cycle time, target, pieces produced, rejects with a reason, good pieces, achievement %, and downtime minutes split by reason (setup, breakdown, tooling, material, QC wait, no operator, power cut, other). Then a day total and a summary of where the time went and why pieces were rejected. OEE is optional, but it comes free once cycle time and downtime are filled in.
How do I calculate achievement % (production efficiency) in a daily report?
+
Achievement % = good pieces ÷ target × 100. In the example, TC-01 shift A made 471 good pieces against a target of 540: 471 ÷ 540 × 100 = 87.2%. Use good pieces, not total produced, because a rejected piece is not output.
What is the difference between achievement % and OEE?
+
Achievement compares output with your plan; OEE compares it with what the machine could ideally make in the planned time. If the target is set below the machine's ideal (TC-01's target of 540 is 90% of the 600 pieces a 45-second cycle allows in 450 minutes), achievement (87.2%) reads higher than OEE (78.5%). Track achievement daily; use OEE to compare machines and find hidden capacity.
Who should fill the daily production report?
+
The operator records pieces, rejects and stops at the machine as they happen; the supervisor checks and totals the sheet at the end of the shift. When a supervisor writes the whole report from memory at the end of the day, short stops disappear and rejects arrive without reasons.
How is a shift report different from a daily production report?
+
A shift report covers one shift and is ready when it ends, so the next shift starts with the facts. The daily production report adds up the day's shifts and compares them with plan. Both should come from the same entries, never typed twice.
Can I use this template in Google Sheets?
+
Yes. Upload the .xlsx to Google Drive and open it with Google Sheets. The formulas and the reason dropdowns work. The coloured bars in the day summary may not carry over; the numbers do.
Does this format work for machines other than CNC?
+
Yes, for any process where you can count pieces and time: lathes, VMCs, HMCs, grinding, presses, injection moulding. Put the ideal cycle time for each job in the cycle-time column and the OEE columns work the same way.
What is an hourly production report?
+
An hourly production report breaks the shift into hours: a target for each hour (the shift target divided by the working hours), the pieces actually made that hour, and the reason whenever an hour falls short. It catches a problem in the hour it happens instead of at the end of the shift. There is a free hourly production report format, with its own Excel template, at opeeye.com/guides/hourly-production-report-format; production tracking software builds it automatically from the same entries.
What is daily production report software?
+
Software that builds the daily production report from entries made at the machine — pieces, rejects with reasons, stops with reasons — instead of from a sheet someone fills in at the end of the shift. The report is ready when the shift ends, short stops are not lost, and the totals, achievement % and OEE are calculated without anyone typing them.
Can the daily production report be generated automatically?
+
Yes. With a tablet at each machine where the operator taps pieces, rejects and stops as they happen, the shift report and the daily production report are produced automatically at the end of each shift. That is what OpeEye does. The Excel and paper versions on this page are for shops that are not there yet.
Can you turn this report into an app for my factory?
+
Yes. The OpeEye team in Rajkot builds production apps around a factory's own format: your columns and reasons, filled on a phone or tablet, with the day's report on WhatsApp. Send a photo of your current register or Excel sheet on WhatsApp to +91 95867 57458 and you get a fixed price before any work starts. CNC and VMC shops can use OpeEye as it is, at ₹399 per machine a month.
Related
- Production trackingPieces vs target per machine, operator, shift and job — without registers.
- Downtime reason codes27 reasons in 8 groups, worded for one-tap logging at the machine.
- How to calculate OEEThe formula, a worked example on a turning centre, and a calculator.
- OEE softwareAvailability × performance × quality, computed from real floor events.